Quality Assurance & Analytical Precision
Ensuring excellence and reliability through rigorous standards, sterile cleanroom environments, advanced chromatography instrumentation, and continuous innovation at Nourqia Health Science.
Batch-by-Batch Analytical Release
HEPA Cleanroom Filtration Zones
Heavy Metal Detection Threshold
Statutory Quality Accreditations
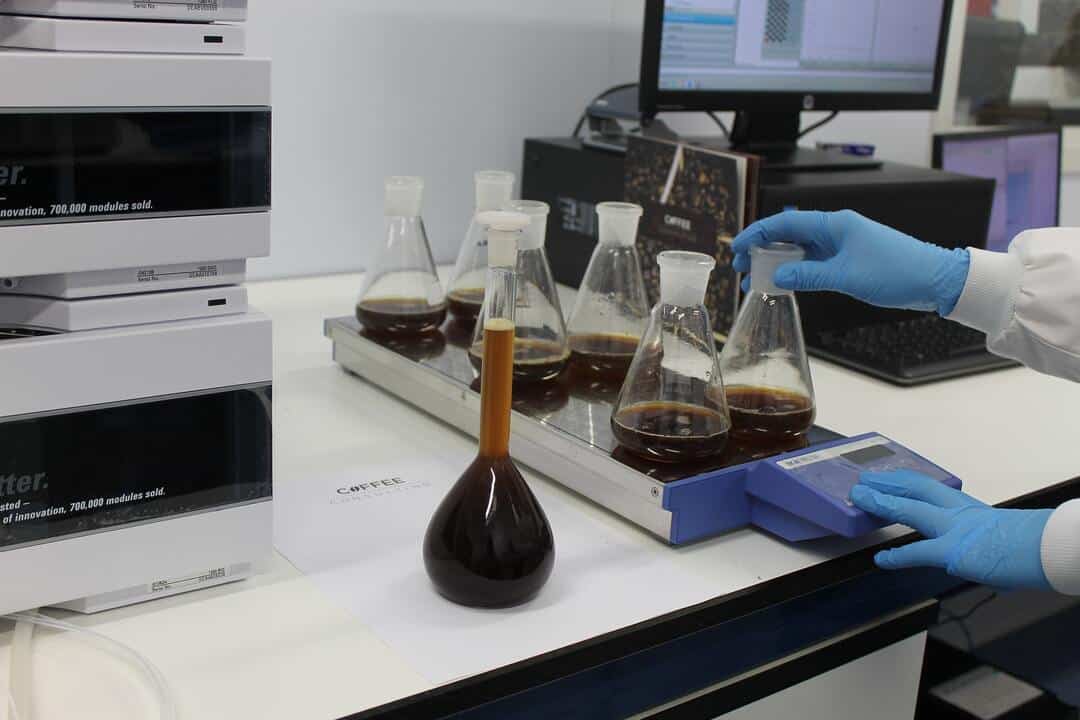
Quality Control
Quality control laboratories conduct comprehensive testing across chemical, physical, and microbiological parameters. Each batch undergoes systematic analysis before release, ensuring products strictly meet established pharmacopoeial specifications and regulatory mandates.
Testing protocols cover stability profiles, active potency verification, impurity screening, and microbial limits—standard assessments that confirm product integrity from manufacturing through complete shelf life. Advanced instrumentation enables detection at levels that support both statutory compliance obligations and clinical efficacy expectations.
Trained analytical chemists follow validated test methods, with results documented, double-checked, and archived as part of mandatory batch disposition processes. This systematic approach provides the unalterable data trail that regulatory inspectors, clinicians, and brand partners demand.
Quality Assurance at Every Stage
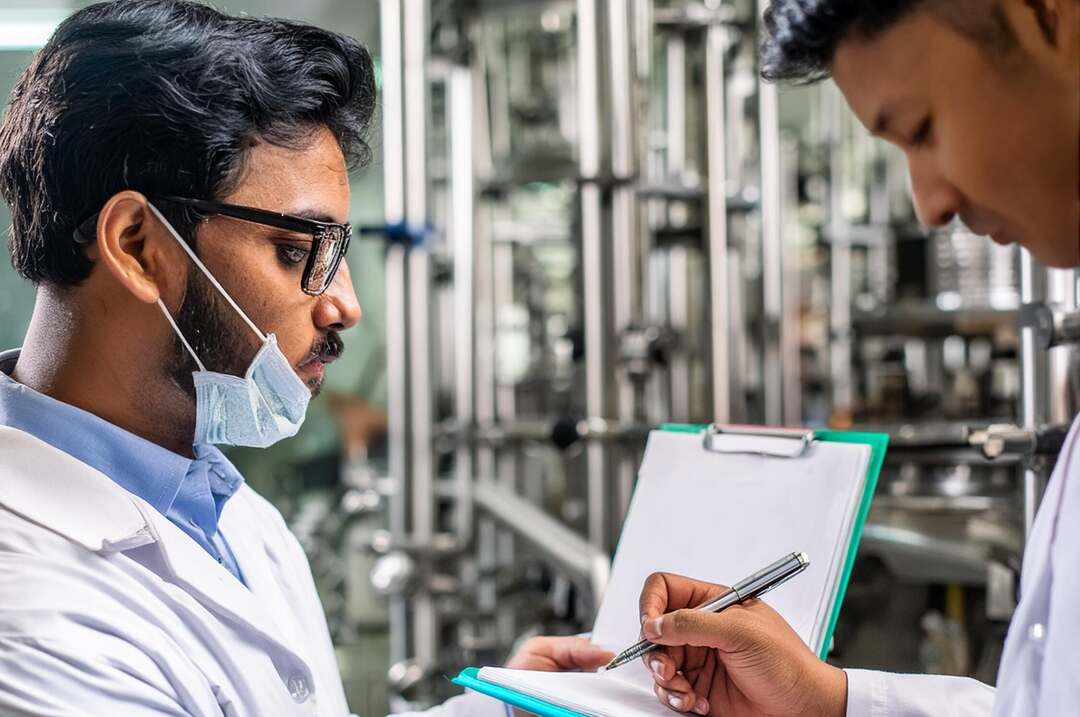
Quality assurance is seamlessly integrated throughout the entire manufacturing process—from incoming raw material quarantine to final finished product dispatch. Each production stage features defined acceptance criteria and documented Standard Operating Procedures (SOPs) that maintain complete uniformity across production cycles.
Incoming ingredients are chemically identified and cleared against raw material specifications before entering dispensing suites. In-process controls (IPC) monitor blend homogeneity, hardness, disintegration time, and fill weights in real time. Finished goods then undergo exhaustive analytical testing before packaging and serialization.
“Our system is designed around a straightforward principle: build quality directly into the process rather than rely solely on end-of-line testing. Prevention is infinitely more effective than correction.”
Maintaining Sterile Environments Throughout
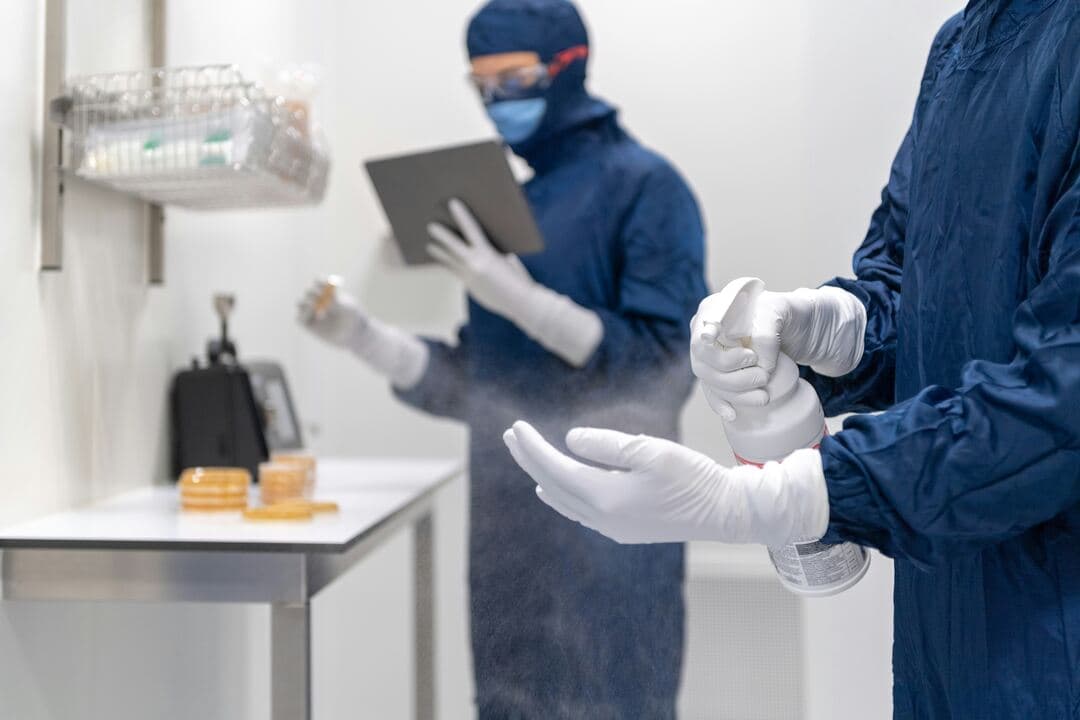
Sterile processing requires strictly controlled environments where airborne particulate counts, viable microbial organisms, differential room pressures, and relative humidity are continuously logged by automated building management systems (BMS).
Our manufacturing suites incorporate cleanroom classifications tailored to product sensitivity—from Class 100,000 secondary suites down to Class 10,000 (ISO Class 7) primary formulation zones. High-Efficiency Particulate Air (HEPA) filtration units maintain 99.97% particulate arrestance at 0.3 microns with positive differential pressure gradients that prevent external ingress.
Personnel adhere to validated multi-stage gowning and air-shower procedures. Formulation equipment undergoes automated Clean-in-Place (CIP) and Sterilize-in-Place (SIP) routines validated by total organic carbon (TOC) surface swab testing between product switches.
Adhering to Regulatory Quality Standards
Product specifications strictly conform to monographs outlined in premier international pharmacopoeias, including the United States Pharmacopeia (USP), British Pharmacopoeia (BP), and Indian Pharmacopoeia (IP), as well as statutory mandates governed by FSSAI.
As analytical technologies advance and global toxicity guidance evolves, our quality governance framework updates testing limits proactively. All procedure revisions undergo formal change control review, cross-functional risk assessment, and document validation prior to implementation.
Regulatory compliance is dynamic, not static. By maintaining continuous regulatory intelligence, routine mock inspections, and full Common Technical Document (CTD) dossiers, Nourqia ensures seamless import authorization and commercial longevity across domestic and overseas healthcare networks.
Utilizing Advanced Analytical Instruments
Formulation precision requires cutting-edge laboratory instrumentation. Our testing facilities are equipped with high-resolution spectrophotometers, chromatography suites, and dissolution units capable of validating chemical identity at parts-per-billion sensitivity.
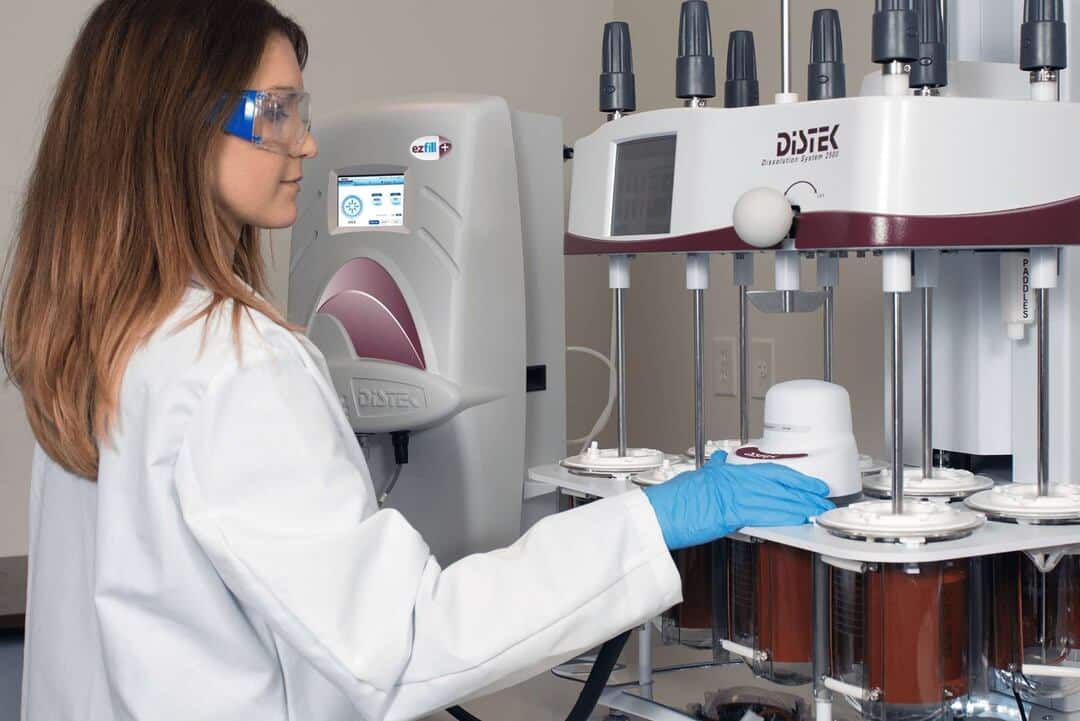
High Performance Liquid Chromatography (HPLC)
Used for high-resolution separation, identification, and microgram quantification of active vitamins, botanical phytonutrients, and amino acid complexes. Validates that every finished batch matches 100% of labeled nutritional claims.
Sub-nanogram sensitivity, quaternary solvent delivery, photodiode array (PDA) detection.
Comprehensive Quality Assurance & Governance
Explore the eight foundational pillars that drive daily manufacturing discipline, hazard prevention, and cross-border compliance at Nourqia Health Science.
International Manufacturing Standards
Engineered according to guidelines established by WHO, PIC/S, and regional authorities including US FDA, ANVISA, and INVIMA.
Facilities and cleanrooms constructed to PIC/S and WHO-GMP specifications.
Comprehensive validation of HVAC air handling systems, water-for-injection (WFI), and automated processing lines.
Strict data integrity systems compliant with 21 CFR Part 11 for electronic batch record archiving.
Clear pathways to global export registration and market licensing across 30+ jurisdictions.
International Manufacturing Accreditations
These accreditations are operational licenses that authorize commercial supply to hospital networks, pharmacy distributors, and healthcare brands worldwide.
WHO-GMP Certified
Rigorous Good Manufacturing Practice validation across all solid, liquid, and powder dosage formats.
EU-GMP Aligned
Aseptic cleanrooms and validated environmental controls meeting stringent European Union market criteria.
FSSAI Licensed
Full central regulatory authorization for high-potency vitamins, minerals, and functional health botanicals.
ISO 9001 & ISO 22000
Global benchmark for total quality management, risk prevention, and food safety governance systems.
HACCP Certified
Systematic physical, chemical, and biological hazard identification throughout every manufacturing phase.
Halal Certified
Ethically compliant, gelatin-free and verified permissible ingredients conforming to international requirements.
Connecting Global Healthcare with Precision Nutraceuticals
We deliver clinical-grade formulations to healthcare providers, hospital networks, and contract partners globally. Our multi-standard certifications (WHO-GMP, FSSAI, ISO, HACCP, Halal) guarantee seamless registration, documented safety, and batch-to-batch therapeutic efficacy.
Technical Dossier Support
Our regulatory affairs team provides complete eCTD / ACTD registration dossiers, stability study data, Free Sale Certificates (FSC), and Certificate of Pharmaceutical Product (CoPP).